Three complete production lines built around JR vibroforming tables and rubber moulds. See exactly how each machine sits on the floor, then choose the plant that fits your output and budget.
3Plant layouts
37+Export countries
1990Established, Kerala
Moulds for every plant
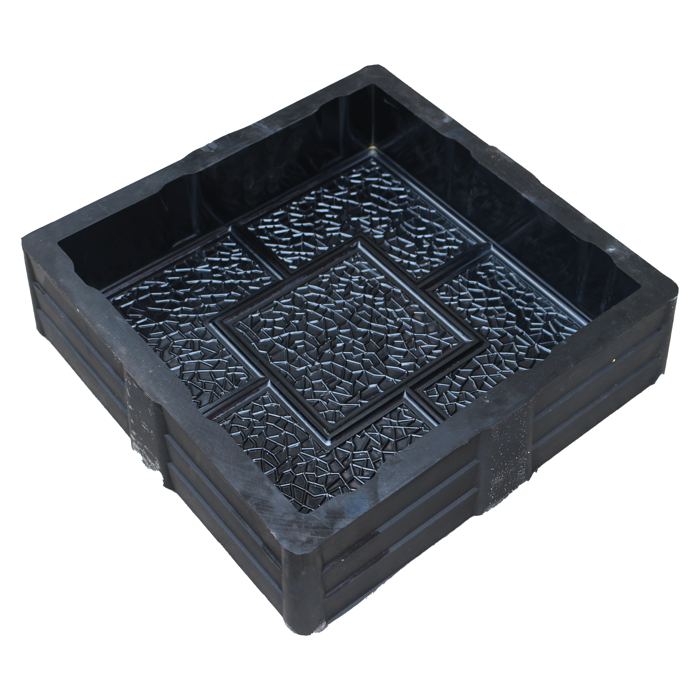
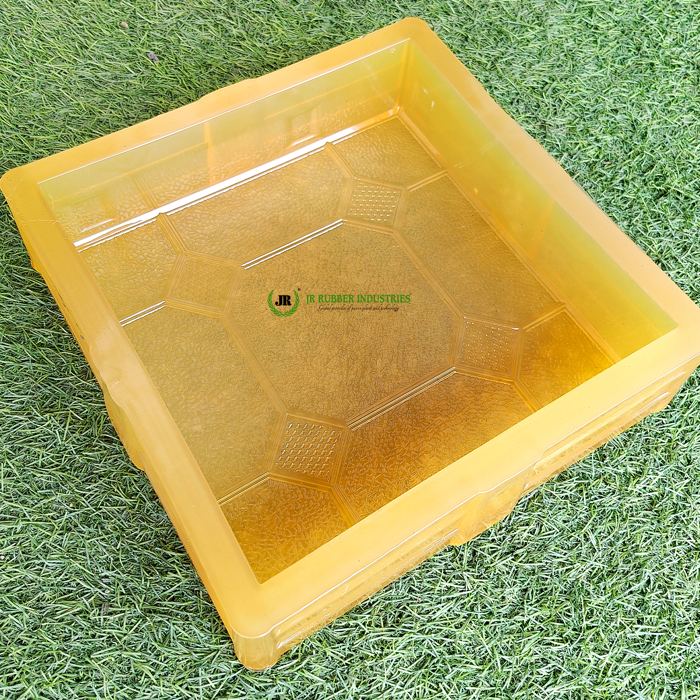
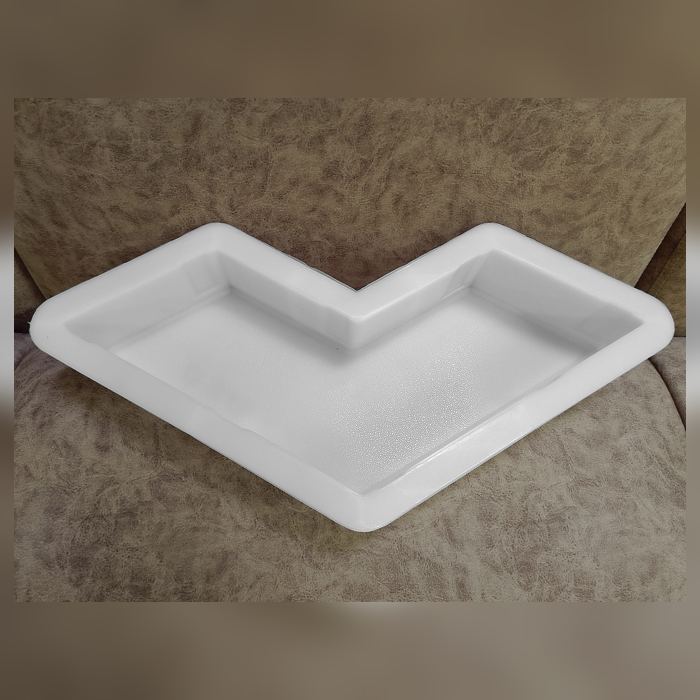
Three kinds of JR moulds
Every JR plant works with rubber, PVC or plastic moulds. Pick the one that suits your products and budget.
Rubber mouldsPVC mouldsPlastic moulds
How a JR line works
From raw mix to finished paver
Colour layer mix
The pan mixer blends cement, fine aggregate and colour oxide for the wear-resistant top face.
Grey concrete mix
The muller-type mixer with hydraulic feed hopper prepares the structural backing layer.
Vibroform
Rubber moulds are filled and compacted on the vibroforming tables, then move along the table automatically.
Demould & cure
Moulds are stacked for curing, demoulded, and returned to the line for the next cycle.
Entry-level
Mini paver plant
A compact, low-investment line for new entrepreneurs. Two vibroforming tables, one colour mixer and one concrete mixer, with a small floor footprint and simple operation.
Works with all 3 JR mould typesRubberPVCPlasticChoose the mould that suits your products and budget.
Higher output
Semi-mechanised paver plant
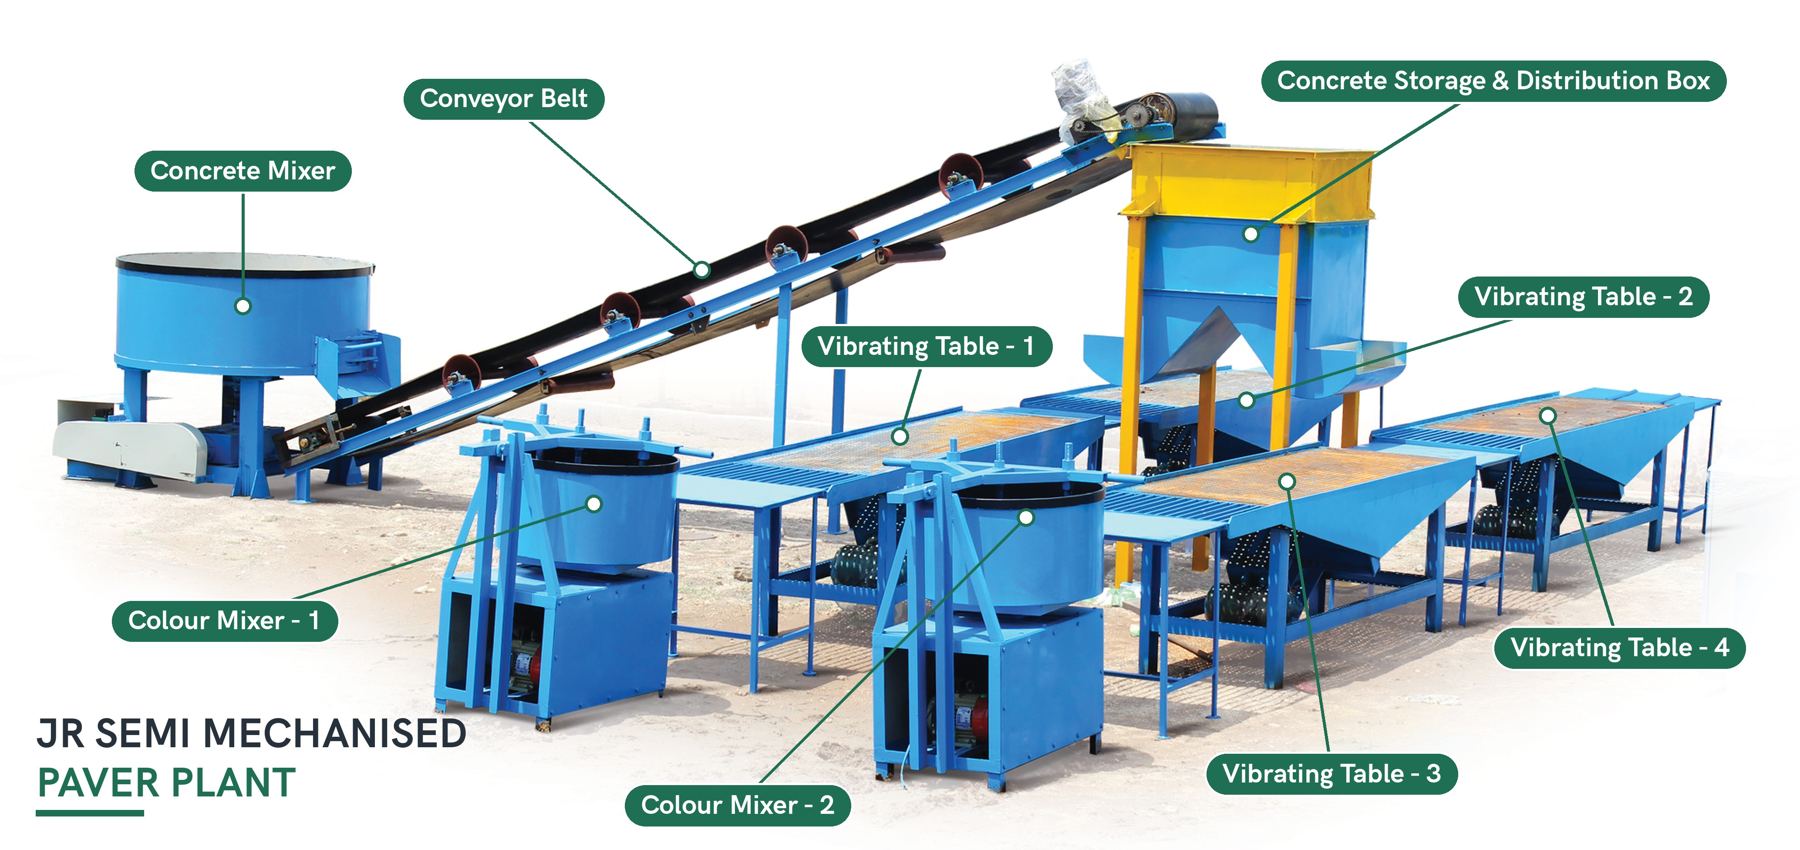
Double the production capacity with less manual handling. A conveyor lifts mixed concrete into a central storage and distribution box that feeds four vibroforming tables.
Large scale
Fully mechanised paver plant
Built for large-scale production, with easy raw material handling. A batching plant, cement feeder and planetary mixer prepare the concrete automatically, and conveyor belts feed two distribution bins serving eight vibrating tables.
Side by side
Which plant fits you?
Feature
Mini paver plant
Semi-mechanised plant
Fully mechanised plant
Vibroforming tables
2
4
8
Colour (pan) mixers
1 × 150 kg/batch, 3 HP
2 × 300 kg/batch, 5 HP
2 × 300 kg/batch, 5 HP
Concrete mixer
Drum rotating type
Muller type, hydraulic hopper, 7.5 HP
Planetary mixer with skip feeder, cement feeder and batching plant
Concrete handling
Manual transfer to tables
20 ft conveyor + 900 L distribution box
Forward and reverse conveyors + 2 distribution bins
Production capacity per plant per 8-hour shift
Approx. 3,500–4,000 nos (120–200 m²)
Approx. 7,000–8,000 nos (240–400 m²)
Approx. 14,000–16,000 nos (480–800 m²)
Best for
New entrepreneurs, local supply, tight budgets
Growing producers serving contractors and larger projects
Large-scale production and major infrastructure supply
Chemicals & colours
Superplasticizer and iron oxides
We supply the chemicals and colours your plant needs, so your pavers come out strong, smooth and evenly coloured from the first batch.
Superplasticizer
A concrete admixture that lets the mix flow into every corner of the mould with less water.
Higher strength: less water gives stronger, denser pavers with faster early strength.
Better flow: fills fine mould details and sharp edges on the vibroforming table.
Smooth finish: fewer air voids and pinholes for a clean, glossy surface.
Even colour: spreads iron oxide evenly for uniform, brighter colours.
Iron oxide colours
High-quality iron oxide pigments for the coloured top layer of pavers and tiles. Supplied in 25 kg bags.
Red110C / 120C / 130C
Yellow313
Black330
Light grey270
Dark grey295
Plan your plant with us
New to paver making? Just tell us your country and your budget, and we will help with everything else: choosing the right plant, the machines, the moulds and setting it up.
Already making pavers and ready to grow? We will help you upgrade to a more efficient plant and make finer products, with new designs and patterns, a smoother finish, richer colours and better quality.